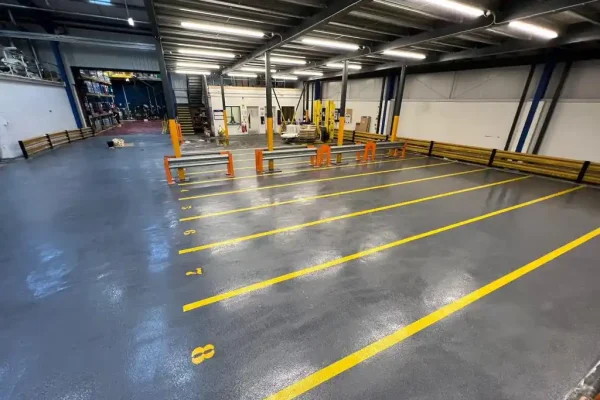
Resin flooring contractors Bolton warehouse and manufacturing operators rely on for floors classified to the traffic they actually carry. Supporting facilities across Logistics North, Wingates, Middlebrook and the older estates at Moses Gate and the inner ring.
Working for national manufacturers, logistics operators and public sector estates since 1999.
As resin flooring contractors Bolton operators call on regularly, we correct under-specification more often than anything else. The town sits on the M61 and M60 logistics spine, and Junctions 4, 5 and 6 have produced large-format distribution floorspace at a scale the eastern boroughs cannot match.
Here the defining factors are floor area, vehicle movement and racking loads. A large-format floor fails when the system chosen is lighter than the traffic crossing it, and no amount of surface hardness compensates for that.
The stock is not uniformly new either. The older estates around Farnworth, Moses Gate and the inner ring carry decades-old concrete with the dusting, joint breakdown and chemical staining that comes with age.
One of the largest logistics developments in the North West, on the M61 corridor south of town.
Established manufacturing and engineering with heavy vehicle movement on the Westhoughton side.
Mixed industrial and commercial units close to Junction 6 of the M61 at Horwich.
Light industrial, trade and storage units with high floor-wear demands on older concrete.
Older industrial and trade premises close to the town centre, typical of the inner ring.
Trade counters and wholesale units where pallet traffic meets customer footfall.
Aisle abrasion, turning circles, racking point loads and dock-edge impact together.
Oil, coolant and solvent exposure alongside static loading under machine bases.
Washdown, thermal shock and hygiene detailing pointing towards polyurethane screeds.
Durability combined with appearance and clearly defined customer routes.
Dock levellers, cage staging and weather ingress at the external transition.
Chemical spillage and the need for a sealed, genuinely cleanable substrate.
A dock apron carries impact, point loading and thermal exposure in the same few metres, and it is the first area to fail in every large-format building we survey. It is specified separately from the main floor, because it is a different problem.
FeRFA Types 1 to 8 and BS 8204-6 separate a high-build coating for pallet traffic from a screed for counterbalance routes.
Dock edges, levellers and the external-to-internal transition need arris protection and joint detailing designed in.
Under HSE L24, forklift routes and crossings are a safety control, and resin survives the traffic where paint does not.
Bolton operators generally install during planned shutdowns rather than stopping for a floor, so the sequence is built backwards from that date and agreed before a system is chosen.
Work is taken aisle by aisle, bay by bay or door by door with racking left loaded where possible, and fast-curing chemistries are used where a zone has to be back under load quickly. Cure behaviour is explained rather than a completion time promised.
On the older estates preparation runs under H-class extraction with areas screened, because aged concrete dusts under traffic and the EH40 limit of 0.1 mg per cubic metre over eight hours applies to the work as much as to the floor.
FeRFA Types 1 to 8 with BS 8204-6, matching build-up to forklift type and racking loads.
Forklift routes, pedestrian segregation and crossings as a control that survives the traffic.
The EH40 limit of 0.1 mg per cubic metre over eight hours where aged concrete dusts under use.
BS 7976 pendulum values in the wet state at wash-throughs, loading areas and food zones.
FeRFA classifies resin flooring into eight types by build-up and thickness, and BS 8204-6 governs which one a floor actually needs, with EN 13813 for the screed. Polyaspartic and MMA sit outside that classification because they describe the resin chemistry rather than the build-up. In Bolton the duty classification is the whole argument.
FeRFA Type 1. Two or more coats up to 150 microns, binding a dusting substrate and giving a cleanable surface. From £8 per square metre.
FeRFA Type 2. Dual component to 300 microns, solvent free, in gloss, matt or silk. Chemical resistance with a decorative finish.
FeRFA Type 3. Up to 1000 microns over prepared concrete and the system specified on most industrial jobs. Takes colour well for demarcation.
FeRFA Type 4. Multi-coat build at 1 to 3mm with aggregate broadcast between coats, for impact and constant wear.
FeRFA Type 5. Flow-applied at 2 to 3mm for a seamless finish where hygiene and cleaning matter more than impact resistance.
FeRFA Type 7. Three part filled system at 4 to 6mm thickness, giving a self-smoothing finish for heavy and very heavy duty areas.
FeRFA Types 7 and 8. Trowel-applied at 6 to 9mm to take thermal shock, steam cleaning and constant heavy forklift traffic.
Cures at temperatures down to −5°C and is ready in around two hours. Installed overnight or at a weekend it can remove the need to shutdown entirely.
Cures in hours, but the odour can taint food, fabrics and stock and the area must be cleared and ventilated. Better suited to new build and refurbishment projects.
Rates run from £8 per square metre for a floor seal to £45 for MMA, inclusive of preparation, labour and materials. Loading bays and dock aprons sit at the upper end and are priced separately, because they take the hardest duty on the site.
| System | FeRFA | Thickness | Per m² |
|---|---|---|---|
| Floor Seal | Type 1 | Up to 150µm | From £8 |
| Epoxy and PU Coating | Type 2 | 150 – 300µm | £8 – £12 |
| High Build Coating | Type 3 | 300 – 1000µm | £8 – £12 |
| Multi-Layer Flooring | Type 4 | 1 – 3mm | £12 – £16 |
| Self-Smoothing | Type 5 | 2 – 4mm | £20 – £30 |
| Heavy Duty Flowable | Type 7 | 4 – 6mm | £25 – £35 |
| Heavy Duty PU Screed | Type 8 | 6 – 9mm | £30 – £40 |
| Polyaspartic | Chemistry | 300 – 500µm | £38 |
| MMA | Chemistry | 2 – 6mm | £45 |
Inclusive of preparation, labour and materials. Rates assume a sound, accessible substrate and are indicative until the floor has been surveyed. Polyaspartic and MMA sit outside the FeRFA type classification because they describe the resin chemistry rather than the build-up.
A three day shutdown at a plant turning over £2,000 an hour is £120,000 of lost output. On most sites that is several times the price of the floor.
Five contractors quoted one timber processing plant. All five proposed the same system and a three to four day closure. None of them costed the closure.
We proposed a faster-curing system installed across a weekend. A higher rate per square metre, and no shutdown at all. On the client’s own figures the avoided losses exceeded the price of the floor.
We install evenings, weekends and one bay at a time.
Whether a shutdown costs you thousands an hour or simply gets in the way, you do not always have to close your site for a resin flooring installation.
Arris rebuilding, crack stitching and flexible sealing across aprons and leveller zones.
Forklift routes, crossings and pedestrian segregation set out as a scheme and laid in resin.
Damp proof membrane where a substrate fails moisture testing, as a standalone package.
Duty-rated systems and joint detailing installed aisle by aisle around live operations.
Oil and coolant resistant floors laid around fixed plant inside shutdown windows.
Dusting inner-ring concrete ground back, sealed and demarcated for current use.
We work across the borough regularly, from Logistics North and Wingates through to Middlebrook at Horwich, Moses Gate at Farnworth, Raikes Lane and the trade units along the A666. We are Cheshire based, so a survey usually happens within days and there is no mobilisation charge for attending.
Usually the system was lighter than the traffic. FeRFA Types 1 to 8 and BS 8204-6 separate a high-build coating suited to pallet trucks from a heavy-duty flowable or screed suited to counterbalance forklifts and racking loads. Specifying on price rather than duty is what shortens the life.
Because they take impact, point loading and thermal exposure at the same time, in the few metres where outside meets inside. Arris protection, joint detailing and the transition itself have to be designed rather than treated as part of the main floor specification.
It lasts, which painted lines on a forklift route do not. Under HSE L24 and the 1992 Workplace Regulations, segregating pedestrians from vehicles is a safety control, and a control that has worn away is not doing its job. Resin marking is built into the floor rather than applied on top.
Yes. Aged concrete releases respirable crystalline silica under traffic, limited under EH40 to 0.1 mg per cubic metre over eight hours, so it is a COSHH duty rather than housekeeping. Sealing the floor stops the generation at source instead of managing the consequences.
From £8 per square metre for a floor seal up to £45 for MMA, inclusive of preparation, labour and materials. Heavy-duty systems for loading bays and forklift routes sit at the upper end. The full table by system is on the cost page.
Tell us what crosses the floor, where the wear is showing and when the shutdown falls. We attend, test the substrate, and put a written specification and a fixed price in front of you at no cost.