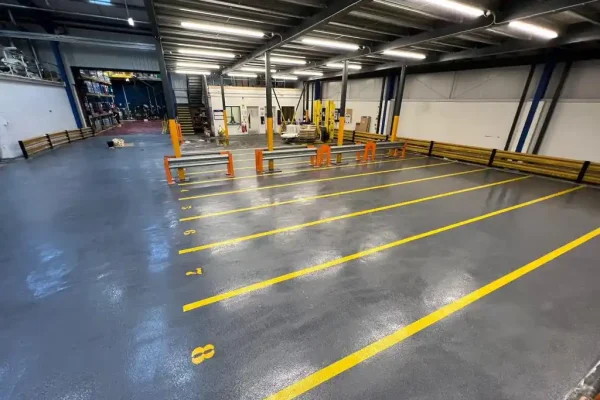
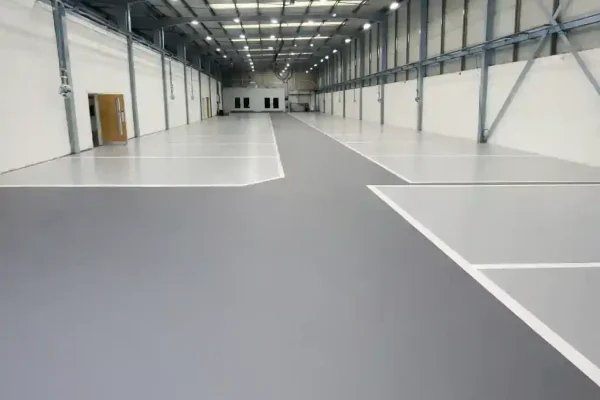
Resin flooring contractors Burnley precision manufacturers and aerospace supply chain businesses rely on for floors specified to a measured standard. Supporting engineering and manufacturing facilities across Network 65, Heasandford, Rossendale Road, Shuttleworth Mead and Burnley Bridge.
Working for national manufacturers, logistics operators and public sector estates since 1999.
As resin flooring contractors Burnley manufacturers call on regularly, we work to requirements a standard warehouse floor cannot meet. The town sits at the eastern end of the M65, with Junctions 9 to 12 serving it and Padiham, and carries the county’s densest concentration of advanced manufacturing and aerospace supply chain work.
That base is technical rather than general. Precision components, tooling, composites, electronics and aerospace-linked work impose controlled particle generation, static dissipation around sensitive assembly and test, and floors flat and strong enough for machine bases and metrology equipment.
It puts Burnley at the opposite end of the county’s specification range from the coast. Here the floor is part of the product quality argument rather than simply a surface that has to survive.
A key East Lancashire employment site with advanced manufacturing beside Junction 9.
Manufacturing and industrial units with heavy machinery use and high floor loads.
Engineering, fabrication and industrial storage facilities across the estate.
Trade and light industrial units with frequent vehicle and pallet traffic.
Modern manufacturing and distribution units at Padiham, west of the town.
Large-format distribution and manufacturing plates with high throughput.
Low particle generation and non-shedding finishes that will not contaminate parts.
Conductive or dissipative build-ups with earthing detail and a tested range.
Point loading under machine feet, vibration at bases and coolant resistance.
Flat, seamless floors with controlled reflectance and stable colour for viewing.
Abrasion and joint protection under continuous forklift movement all day.
Coved, falled, non-porous detailing with washdown and cleaning resistance.
Static control is a tested, earthed system rather than a property of a coating. EN 1081 provides the measurement basis, and conductive and dissipative describe different resistance ranges. A quotation that says anti-static without a value has not specified anything.
Resistance stated as a range with test conditions, and earthing forming part of the system.
Next to controlled areas the argument is particle generation, seamlessness and coved junctions.
Static and dynamic loads from plant and racking push these floors into heavier build-ups.
Machine bases are fixed and inspection schedules are not ours to move, so sequencing is agreed against production and audit dates rather than proposed around our availability.
Work is taken bay by bay or cell by cell, with detailing formed up to machine bases and plinths rather than stopping short of them. Where polyurethane systems are used, ISOPA and ALIPA diisocyanate training records apply and every operative holds current REACH certification.
Preparation runs under H-class extraction with areas screened. Machining already contributes airborne dust in these halls, and the EH40 limit of 0.1 mg per cubic metre over eight hours applies to our works as much as to yours.
The measurement basis for conductive and dissipative floors, with earthing as part of it.
FeRFA Types 6 to 8 framed against BS 8204-6 and EN 13813 for machine and racking loads.
The EH40 limit of 0.1 mg per cubic metre where machining already generates airborne dust.
BS 7976 pendulum values specified for oil and coolant rather than for water alone.
FeRFA classifies resin flooring into eight types by build-up and thickness, and BS 8204-6 governs which one a floor actually needs, with EN 13813 for the screed and EN 1081 where electrical resistance is required. Polyaspartic and MMA sit outside that classification because they describe the resin chemistry rather than the build-up. In Burnley the requirement is usually written down before we arrive.
FeRFA Type 1. Two or more coats up to 150 microns, binding a dusting substrate and giving a cleanable surface. From £8 per square metre.
FeRFA Type 2. Dual component to 300 microns, solvent free, in gloss, matt or silk. Chemical resistance with a decorative finish.
FeRFA Type 3. Up to 1000 microns over prepared concrete and the system specified on most industrial jobs. Takes colour well for demarcation.
FeRFA Type 4. Multi-coat build at 1 to 3mm with aggregate broadcast between coats, for impact and constant wear.
FeRFA Type 5. Flow-applied at 2 to 3mm for a seamless finish where hygiene and cleaning matter more than impact resistance.
FeRFA Type 7. Three part filled system at 4 to 6mm thickness, giving a self-smoothing finish for heavy and very heavy duty areas.
FeRFA Types 7 and 8. Trowel-applied at 6 to 9mm to take thermal shock, steam cleaning and constant heavy forklift traffic.
Cures at temperatures down to −5°C and is ready in around two hours. Installed overnight or at a weekend it can remove the need to shutdown entirely.
Cures in hours, but the odour can taint food, fabrics and stock and the area must be cleared and ventilated. Better suited to new build and refurbishment projects.
Rates run from £8 per square metre for a floor seal to £45 for MMA, inclusive of preparation, labour and materials. Static-controlled and heavy-duty machine areas sit at the upper end, and are specified only where the process requires them.
| System | FeRFA | Thickness | Per m² |
|---|---|---|---|
| Floor Seal | Type 1 | Up to 150µm | From £8 |
| Epoxy and PU Coating | Type 2 | 150 – 300µm | £8 – £12 |
| High Build Coating | Type 3 | 300 – 1000µm | £8 – £12 |
| Multi-Layer Flooring | Type 4 | 1 – 3mm | £12 – £16 |
| Self-Smoothing | Type 5 | 2 – 4mm | £20 – £30 |
| Heavy Duty Flowable | Type 7 | 4 – 6mm | £25 – £35 |
| Heavy Duty PU Screed | Type 8 | 6 – 9mm | £30 – £40 |
| Polyaspartic | Chemistry | 300 – 500µm | £38 |
| MMA | Chemistry | 2 – 6mm | £45 |
Inclusive of preparation, labour and materials. Rates assume a sound, accessible substrate and are indicative until the floor has been surveyed. Polyaspartic and MMA sit outside the FeRFA type classification because they describe the resin chemistry rather than the build-up.
A three day shutdown at a plant turning over £2,000 an hour is £120,000 of lost output. On most sites that is several times the price of the floor.
Five contractors quoted one timber processing plant. All five proposed the same system and a three to four day closure. None of them costed the closure.
We proposed a faster-curing system installed across a weekend. A higher rate per square metre, and no shutdown at all. On the client’s own figures the avoided losses exceeded the price of the floor.
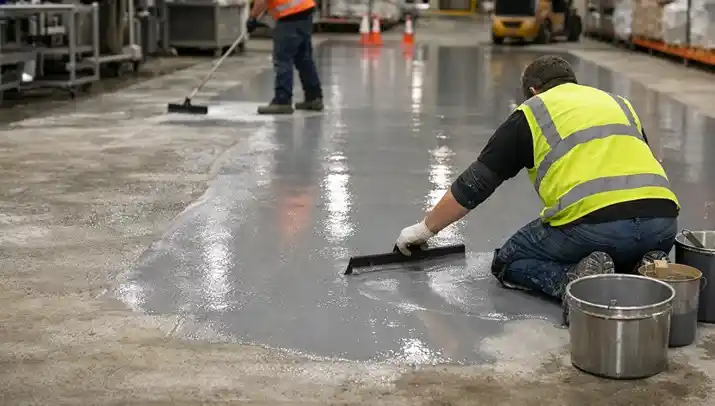
We install evenings, weekends and one bay at a time.
Whether a shutdown costs you thousands an hour or simply gets in the way, you do not always have to close your site for a resin flooring installation.
Copper strip, connection points and continuity installed as part of a dissipative system.
Making good and detailing up to plinths, feet and bases without stopping short.
Damp proof membrane where a substrate fails moisture testing, as a standalone package.
Non-shedding seamless finishes with resistance values recorded for the specification.
Heavy-duty build-ups under machine bases with coolant and swarf resistance.
Abrasion resistant floors and joint repairs across the distribution stock.
We work across the area regularly, from Network 65 at Junction 9 and Heasandford through to Rossendale Road, Burnham Gate, Shuttleworth Mead at Padiham and Burnley Bridge at Hapton. We are Cheshire based, so a survey usually happens within days and there is no mobilisation charge for attending.
Resistance range, and it matters. EN 1081 provides the measurement basis, and the two describe different bands rather than being interchangeable. A floor should be specified with the range required, the test conditions and the earthing detail, because a coating on its own controls nothing.
We install seamless, non-shedding, coved systems suited to controlled and cleanroom-adjacent areas, and we state exactly what the system does. We do not claim a cleanroom classification on your behalf, because that belongs to your validation process rather than to a flooring contractor.
Because static and dynamic loads concentrate at the base. Machine feet and racking baseplates put weight through very small areas and vibration works on it continuously, which pushes the answer into the heavier FeRFA build-ups rather than a coating chosen on wear figures.
One measured against oil, not water. Coolant and cutting oil behave very differently from water underfoot, so BS 7976 pendulum testing should be specified for the actual contaminant. A wet-tested value tells you very little about a floor with coolant on it.
From £8 per square metre for a floor seal up to £45 for MMA, inclusive of preparation, labour and materials. Static-controlled and heavy-duty systems sit at the upper end. The full table by system is on the cost page.
Nelson · Accrington · Blackburn · Chorley · Preston · Leyland · Skelmersdale
Tell us what the area produces, what it must do electrically and what the machines put through the floor. We attend, test the substrate, and put a written specification and a fixed price in front of you at no cost.